Incoming coil
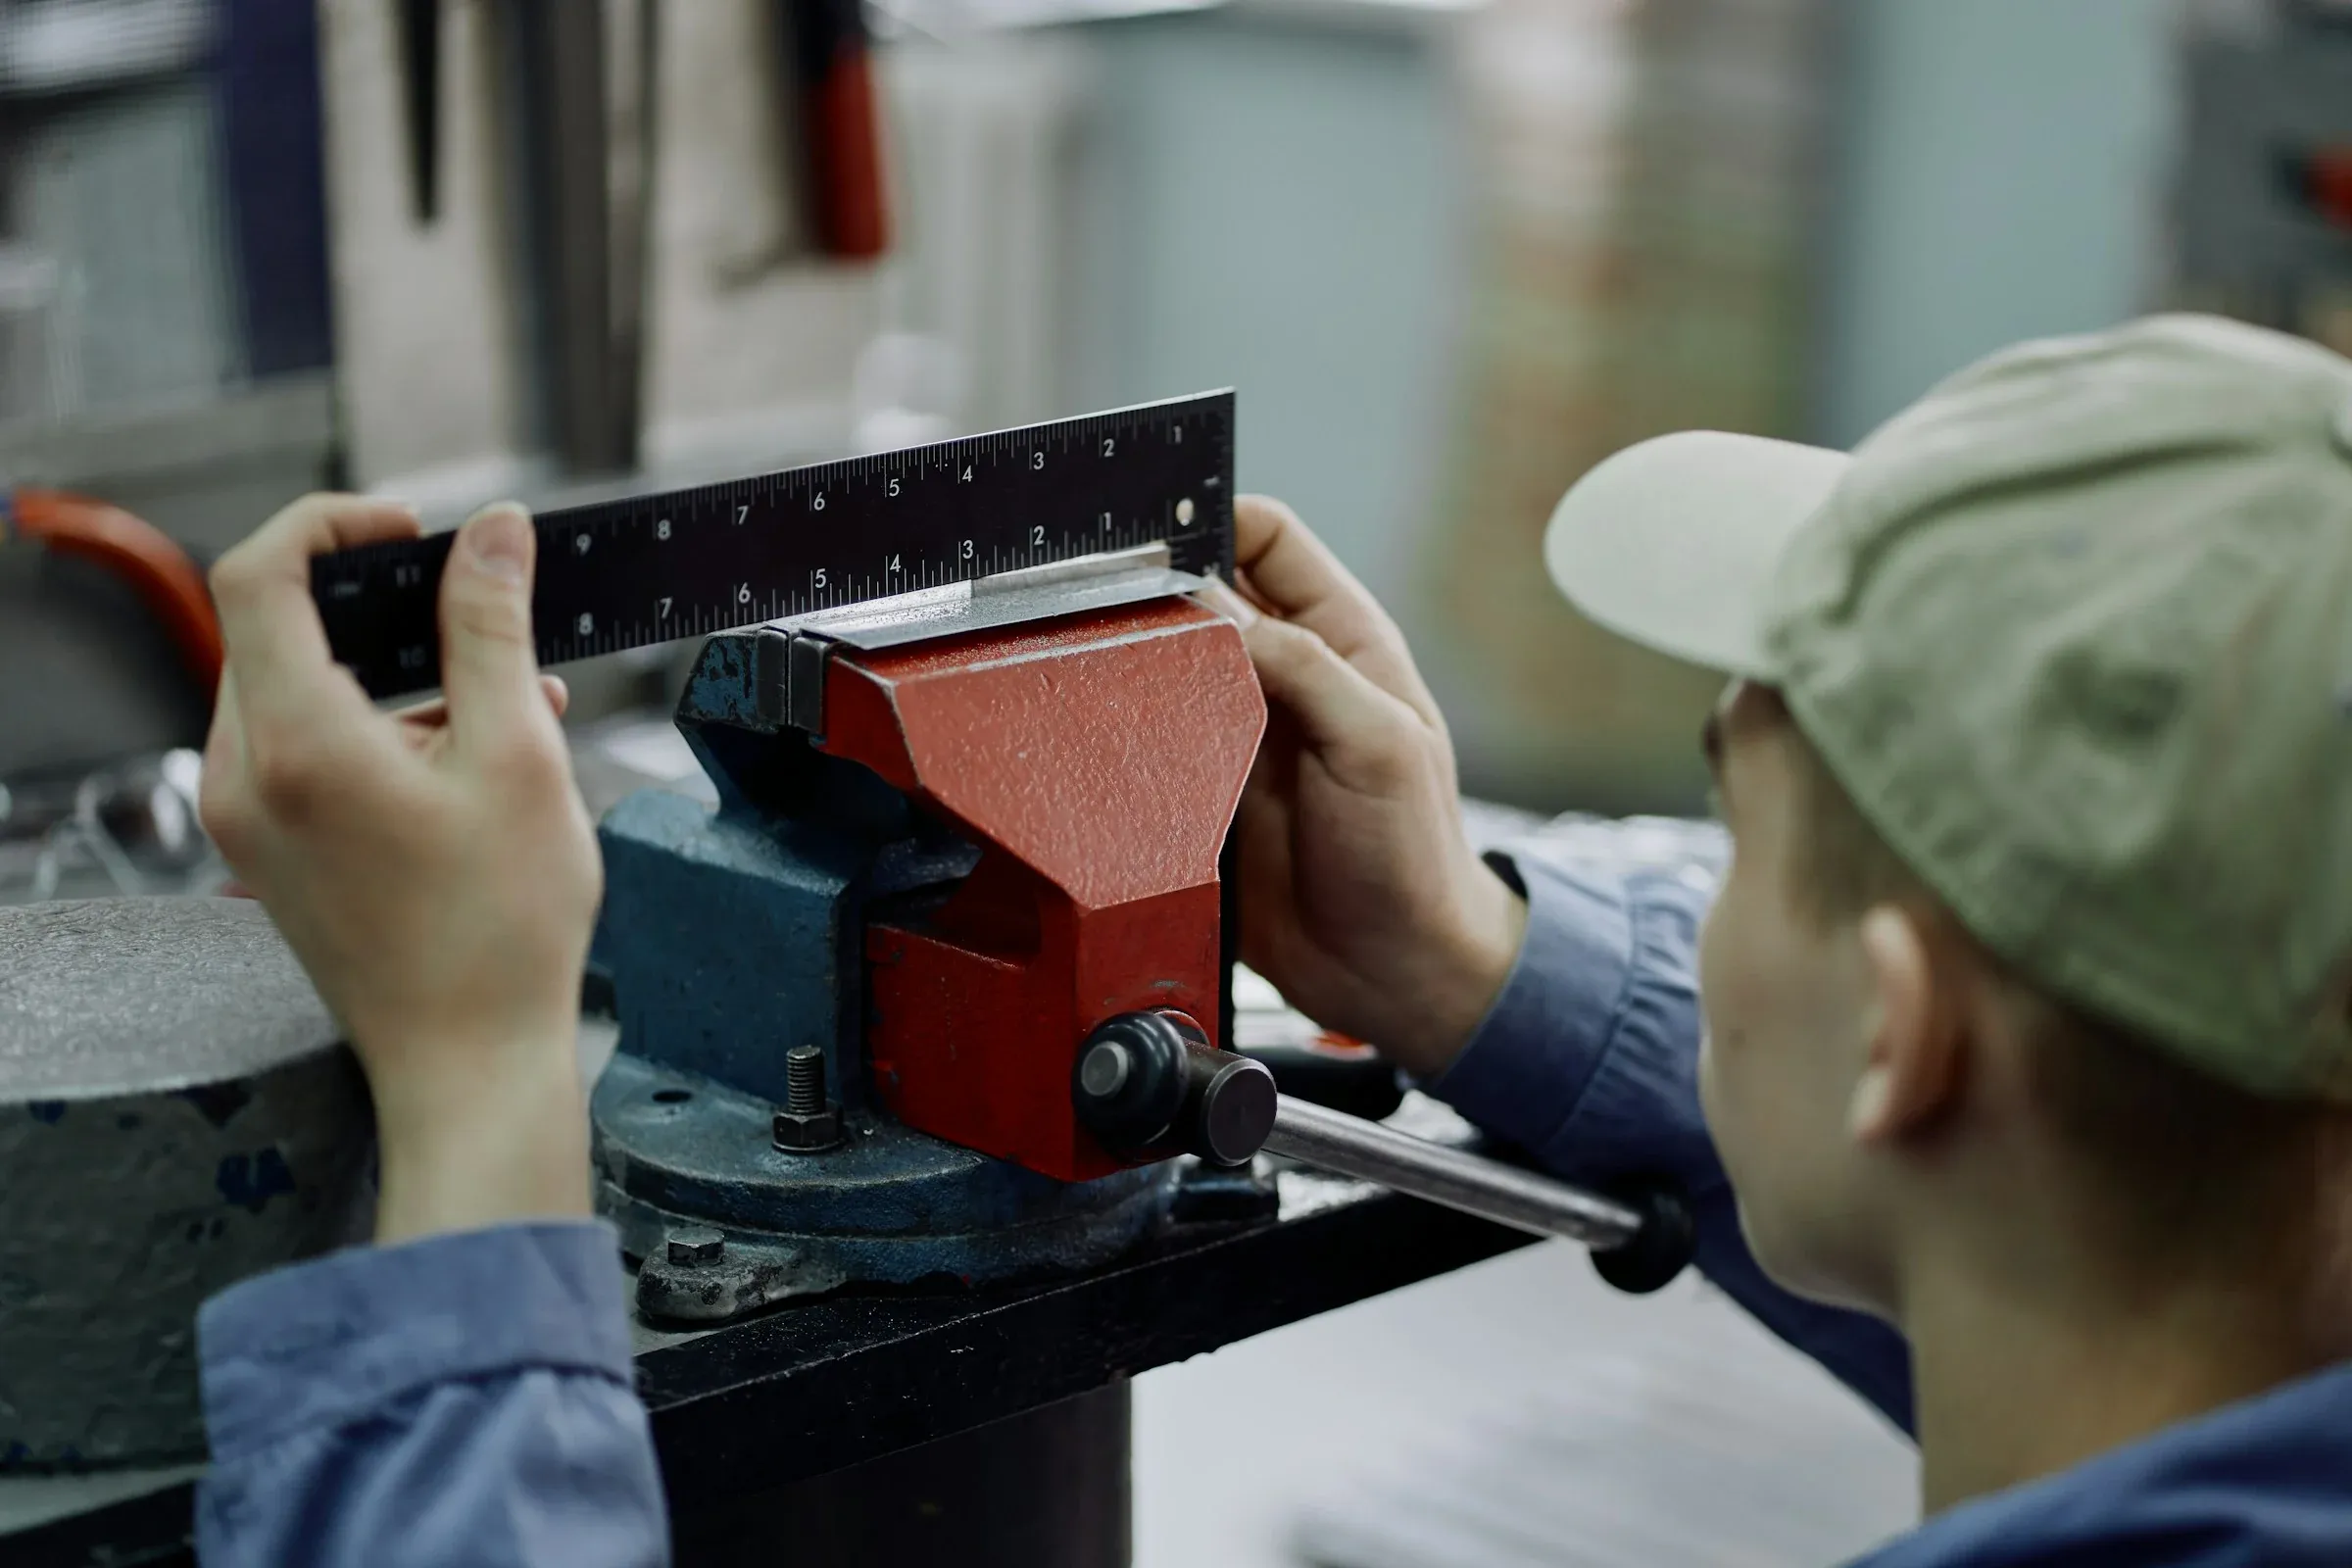
Gauge, width and surface checked on every coil before it is accepted. Non-conforming stock is rejected at the gate, not on the line.
Quality & standards
Sun Steel manufactures to published international specifications and tests against them. Here is what is checked, and where.
Quality & standards
Where a project calls for a standard not listed, tell us at enquiry — we produce against JIS, DIN, EN, BS, ISO and PS on order.
Inspection
Gauge, width and surface checked on every coil before it is accepted. Non-conforming stock is rejected at the gate, not on the line.
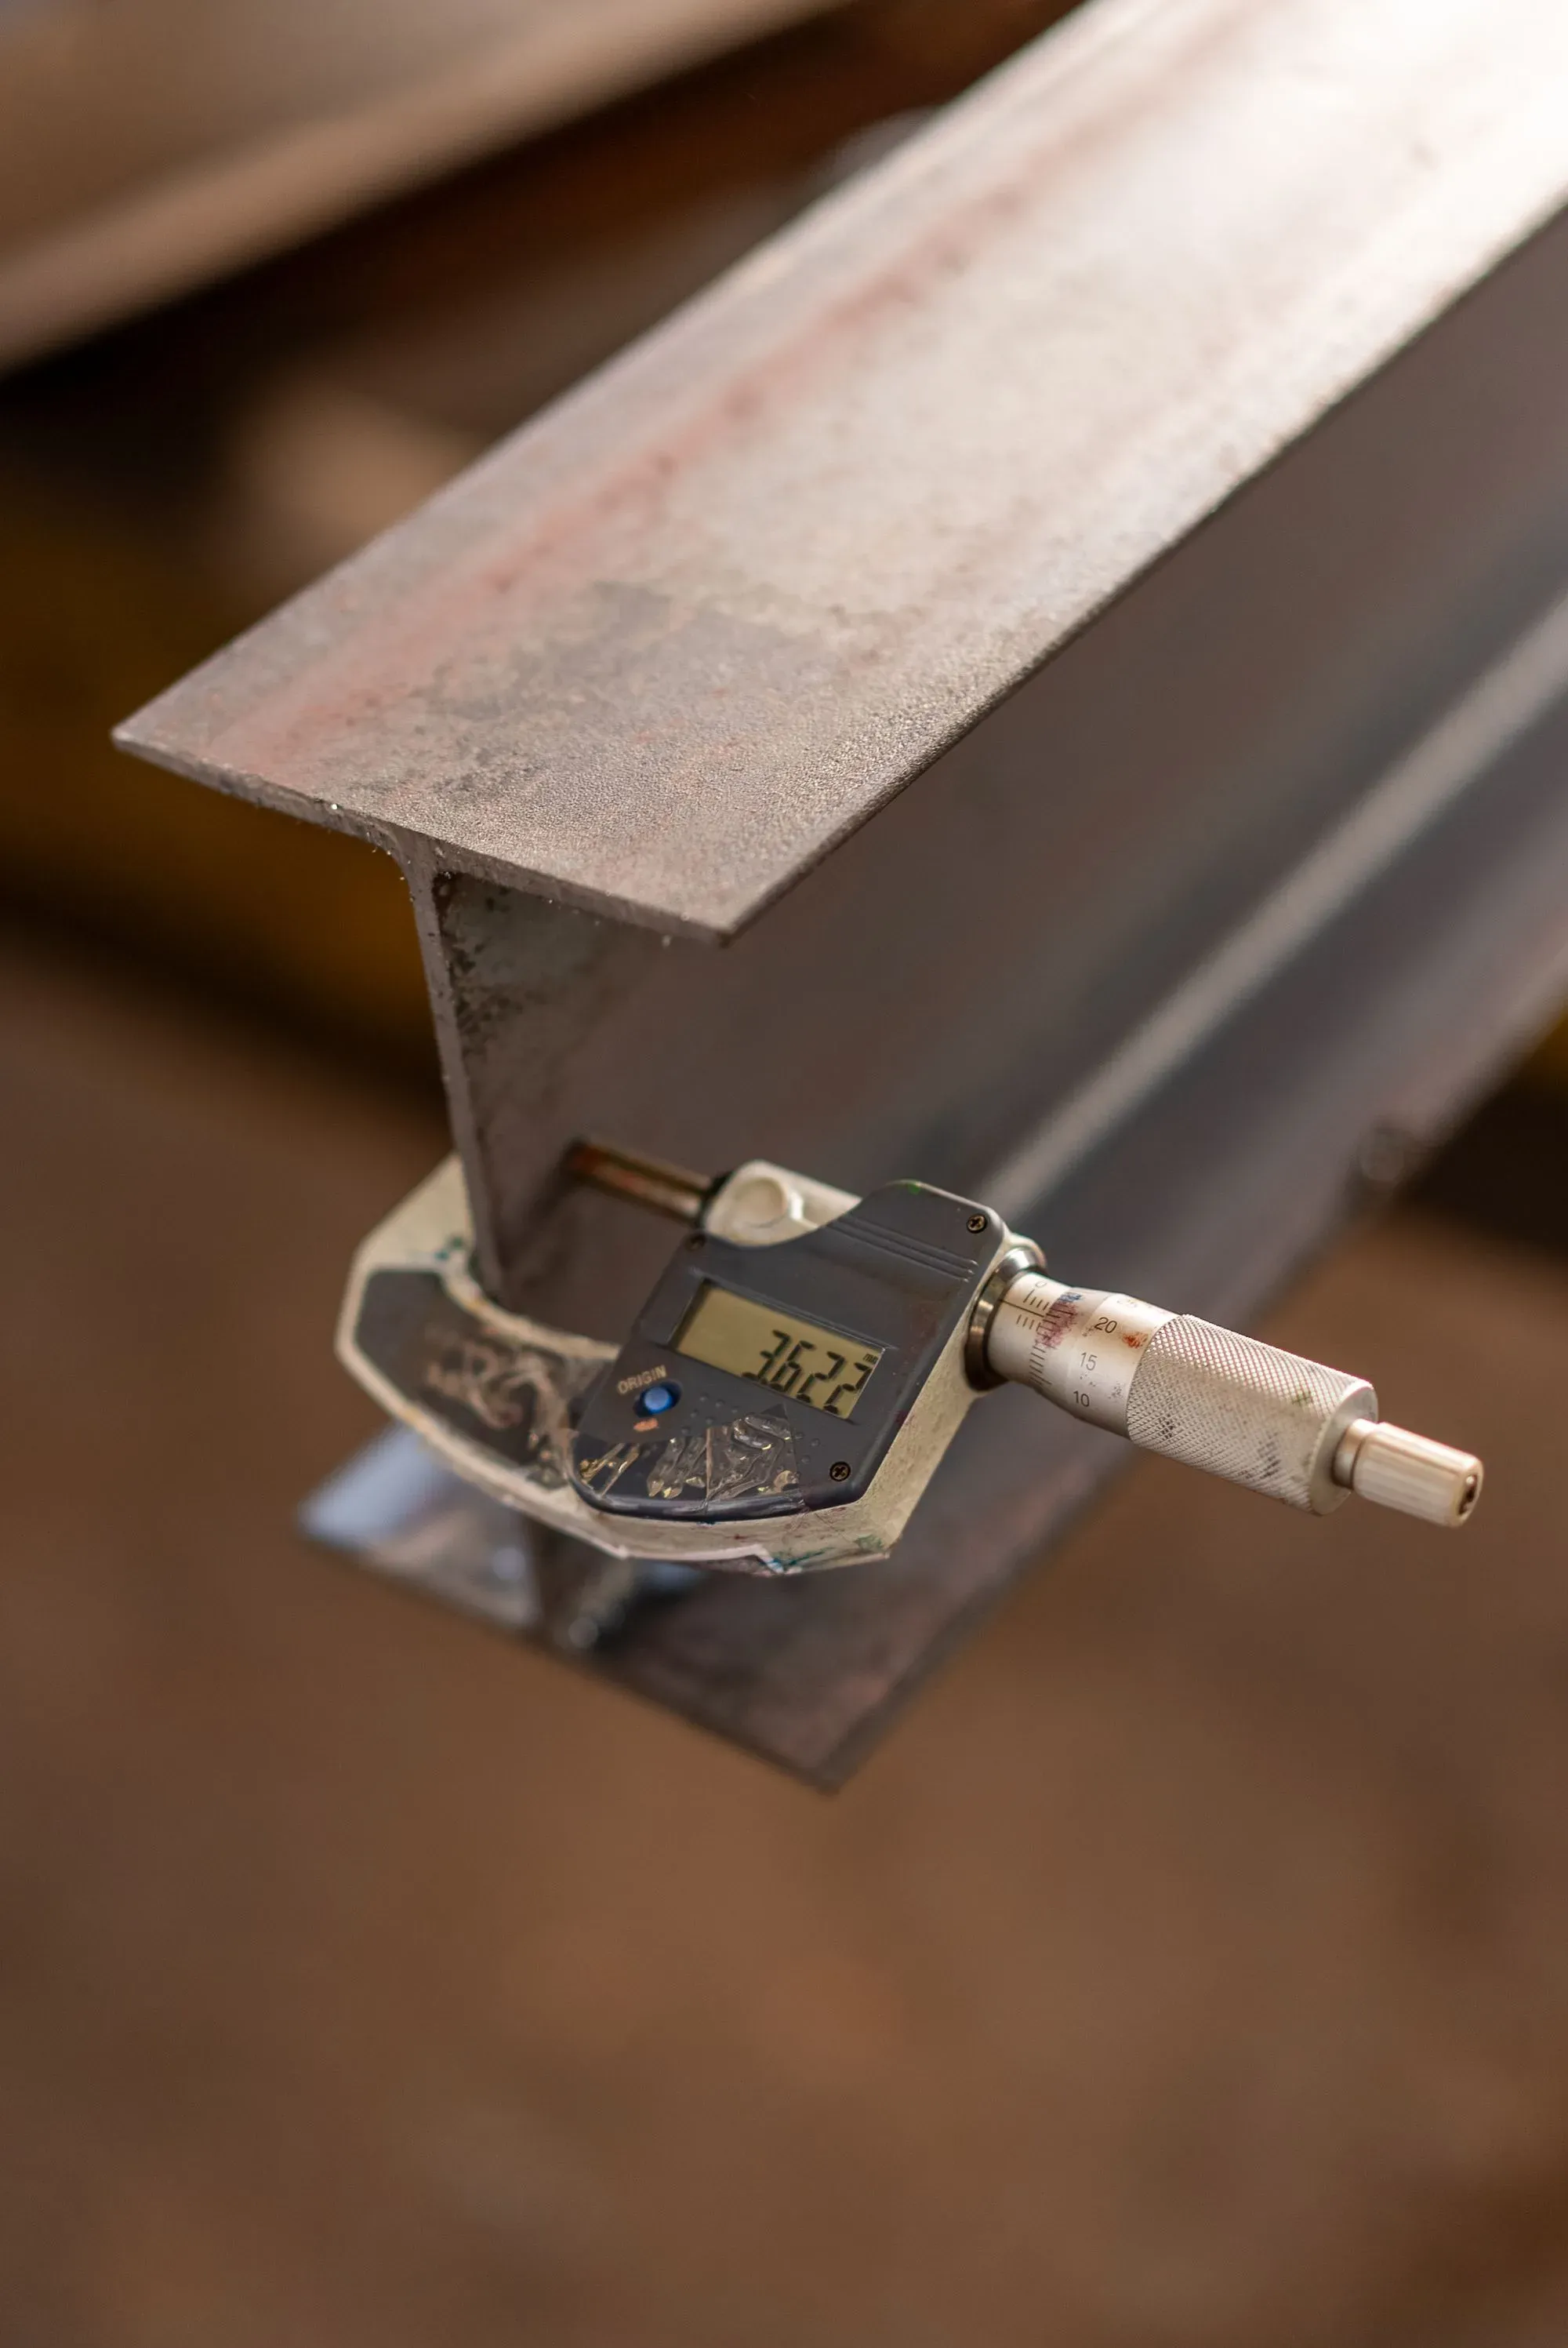
Thickness taken across the width and along the length, against the tolerance band of the governing standard — not once at the head end.
Zinc weight and adherence proved on galvanized stock; paint thickness and adhesion on pre-painted. Both quoted across the two faces.
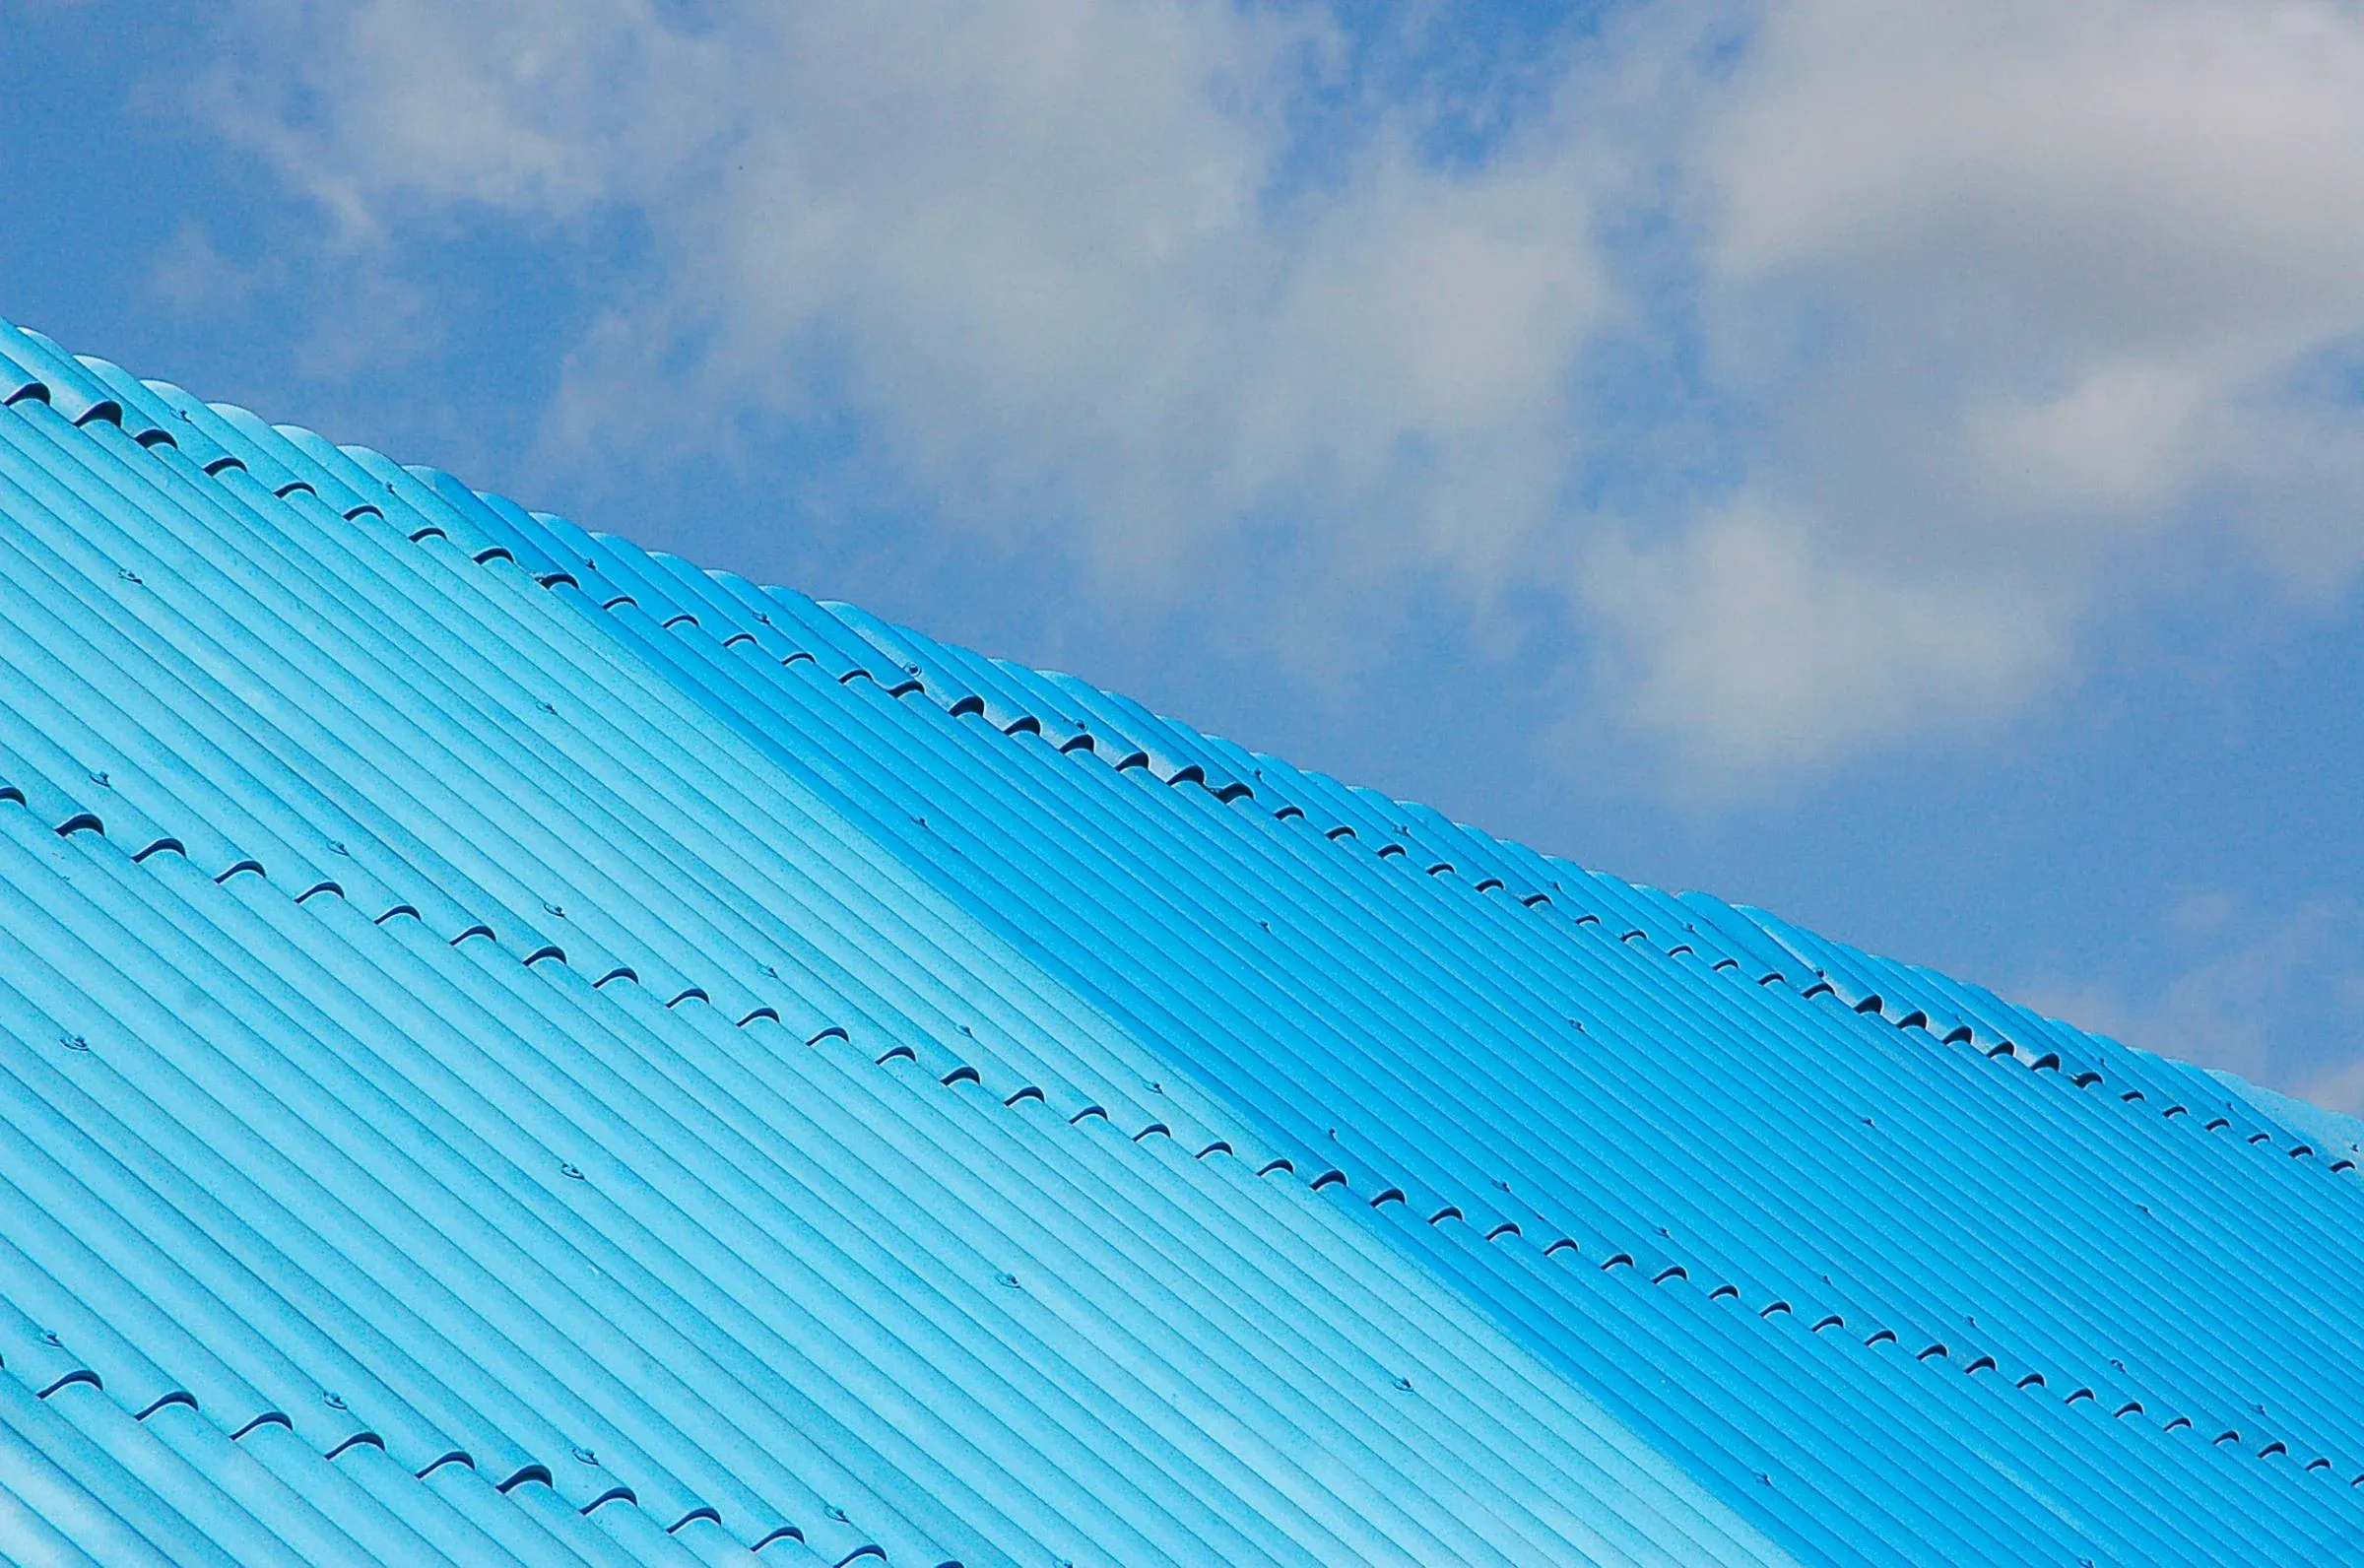
Rolled sections measured on cover width and rib height against the profile drawing, because cover is what a roof is quoted on.
Drawn wire gauged along the coil and pulled for tensile and elongation, with the millimetre governing rather than the gauge number.
A mill certificate is raised for the consignment and travels with it. Third-party inspection accommodated on request.
In-house testing facilities
Testing sent out is testing that waits for a slot and comes back a week later. Every one of these machines is on site, which is what lets a consignment be proved and released in the same week it is rolled.
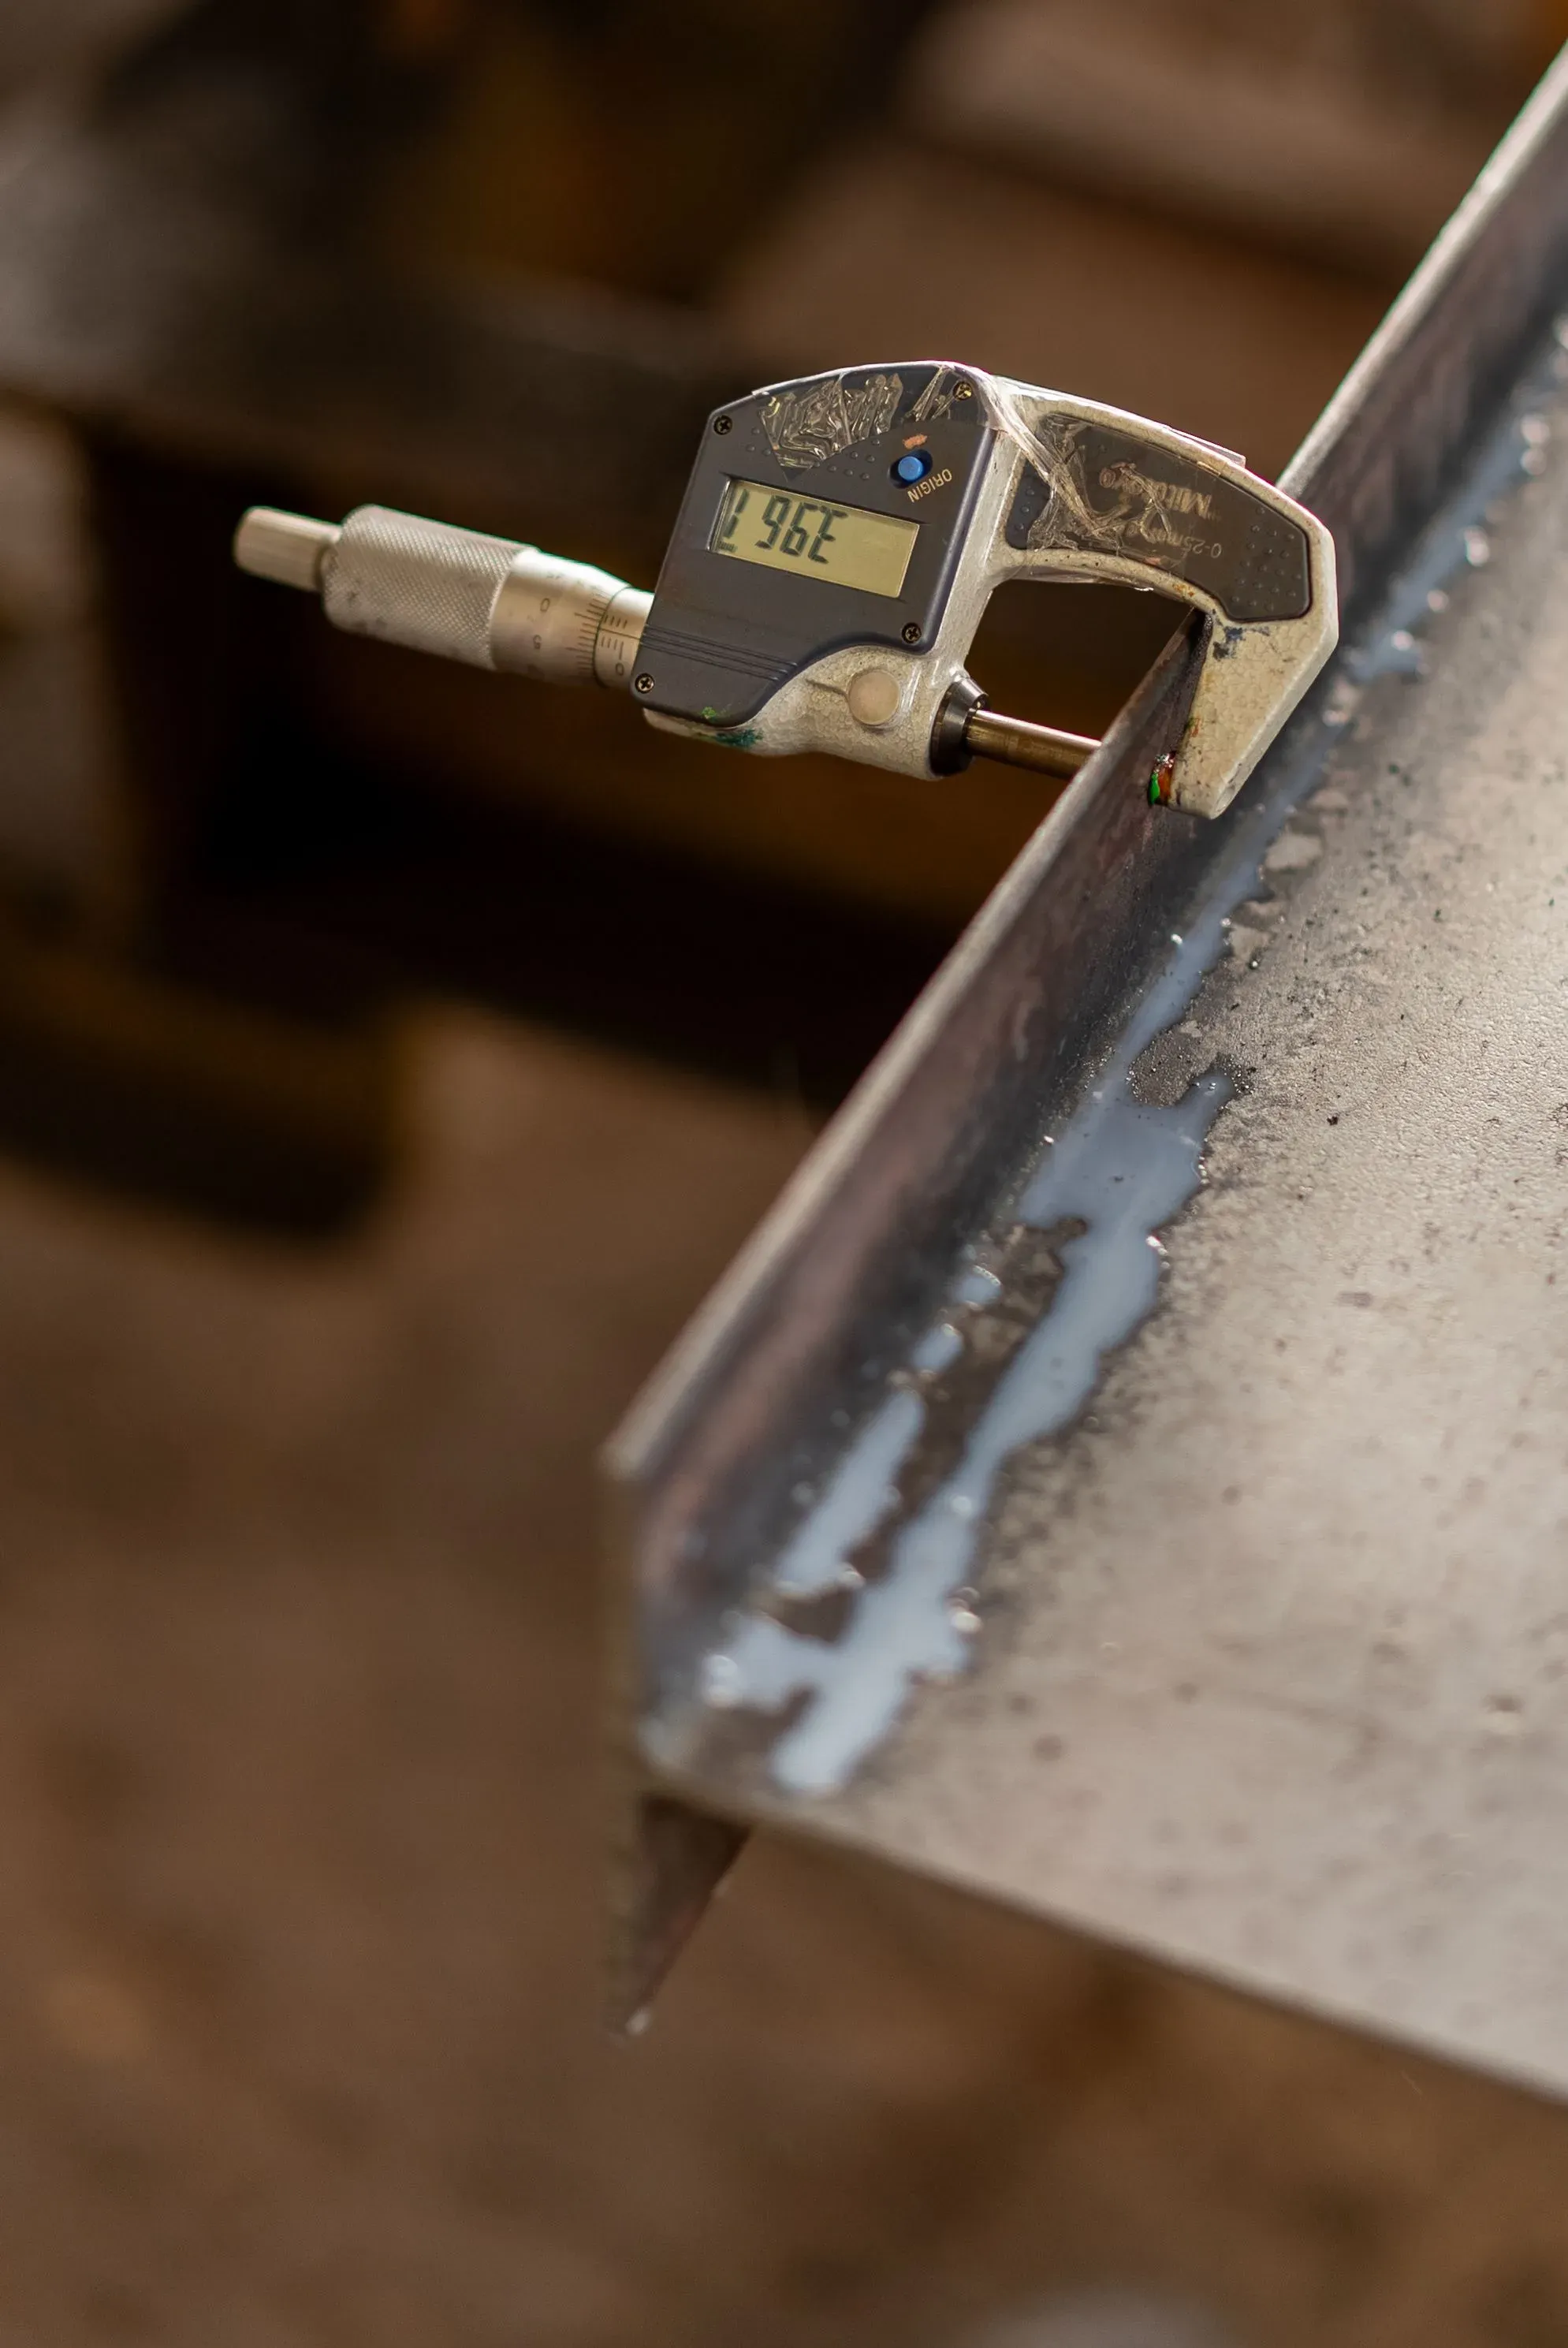
Sheet thickness is taken with a digital micrometer across the width and through the coil, not once at the head end. On coated stock the reading is the ordered thickness, which includes the zinc — the base metal underneath is thinner, and the charts say by how much.
Coating weight is proved by the standard methods rather than taken on trust: copper sulphate for adherence and uniformity, and mass by weight across both faces. Coatings run Z40 to Z275 and are quoted as the total of the two surfaces.
Pre-painted sheet is bent through a T-bend and the coating checked for cracking or lift at the radius. A paint system that fails here fails on site the first time a fabricator folds a flashing.
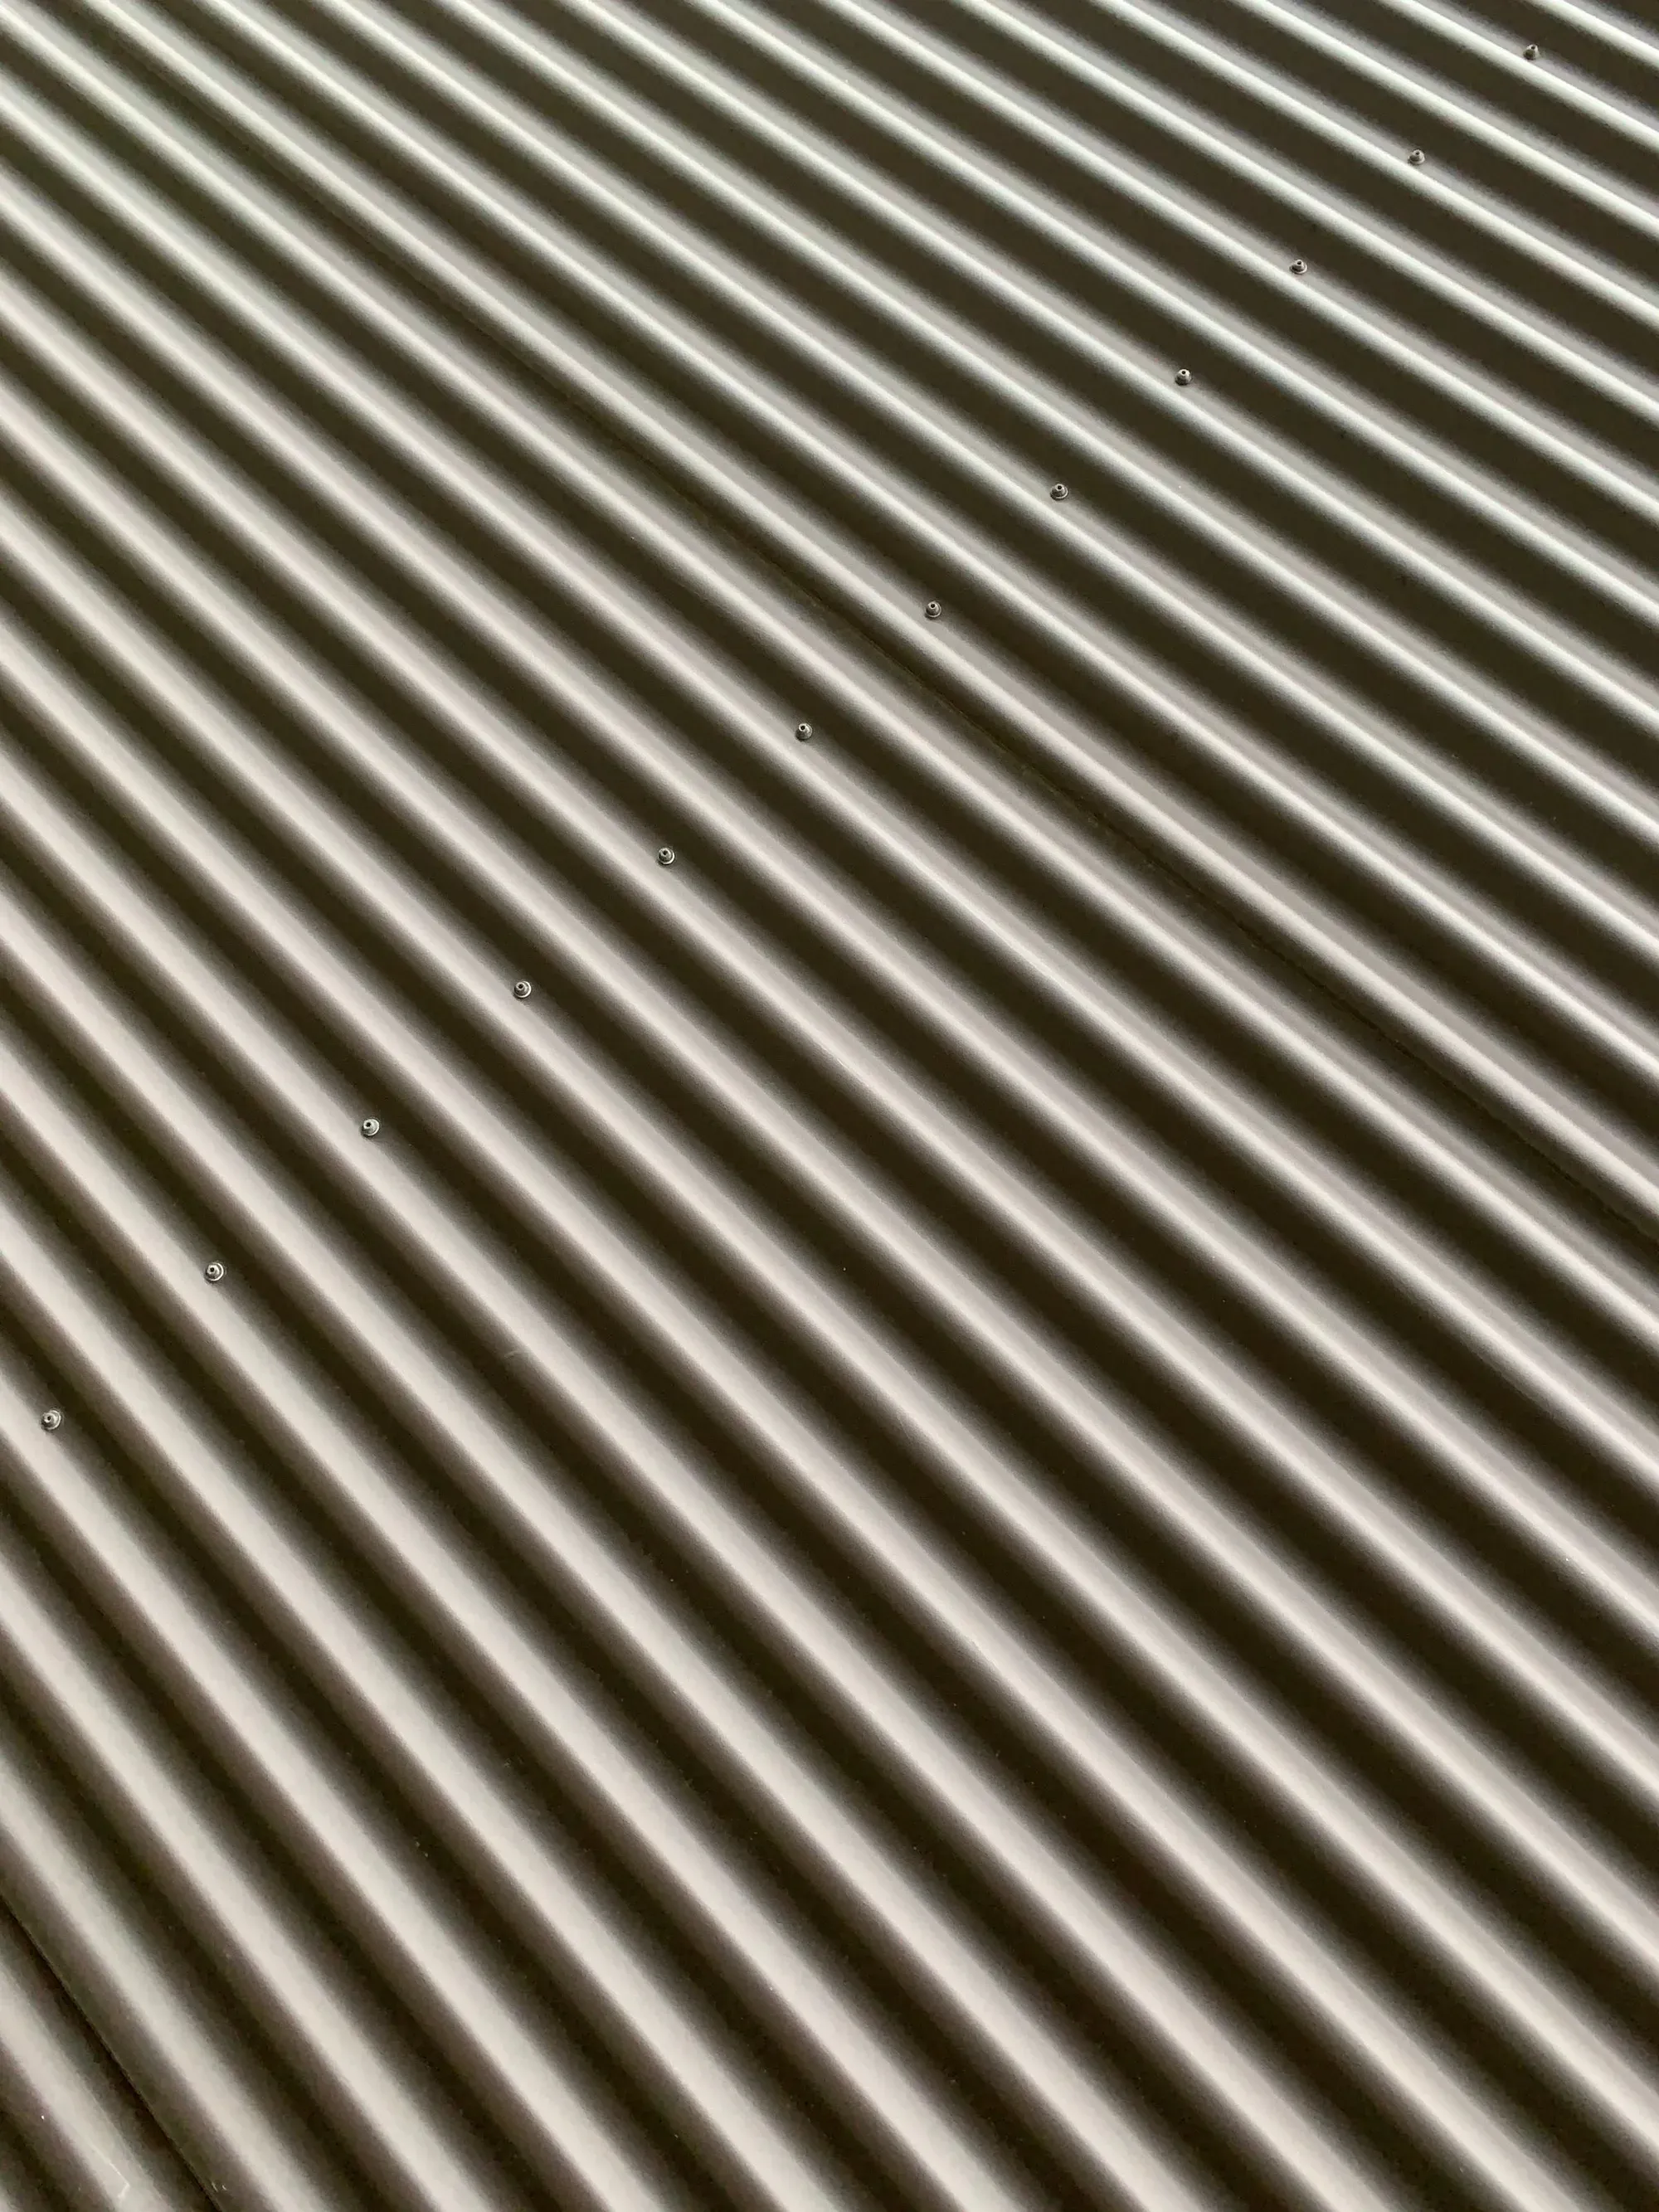
Rolled sections are measured on cover width, not overall width, and the rib height checked against the profile drawing. Cover is what a sheet actually covers once side-lapped, and it is what a roof is quoted on.
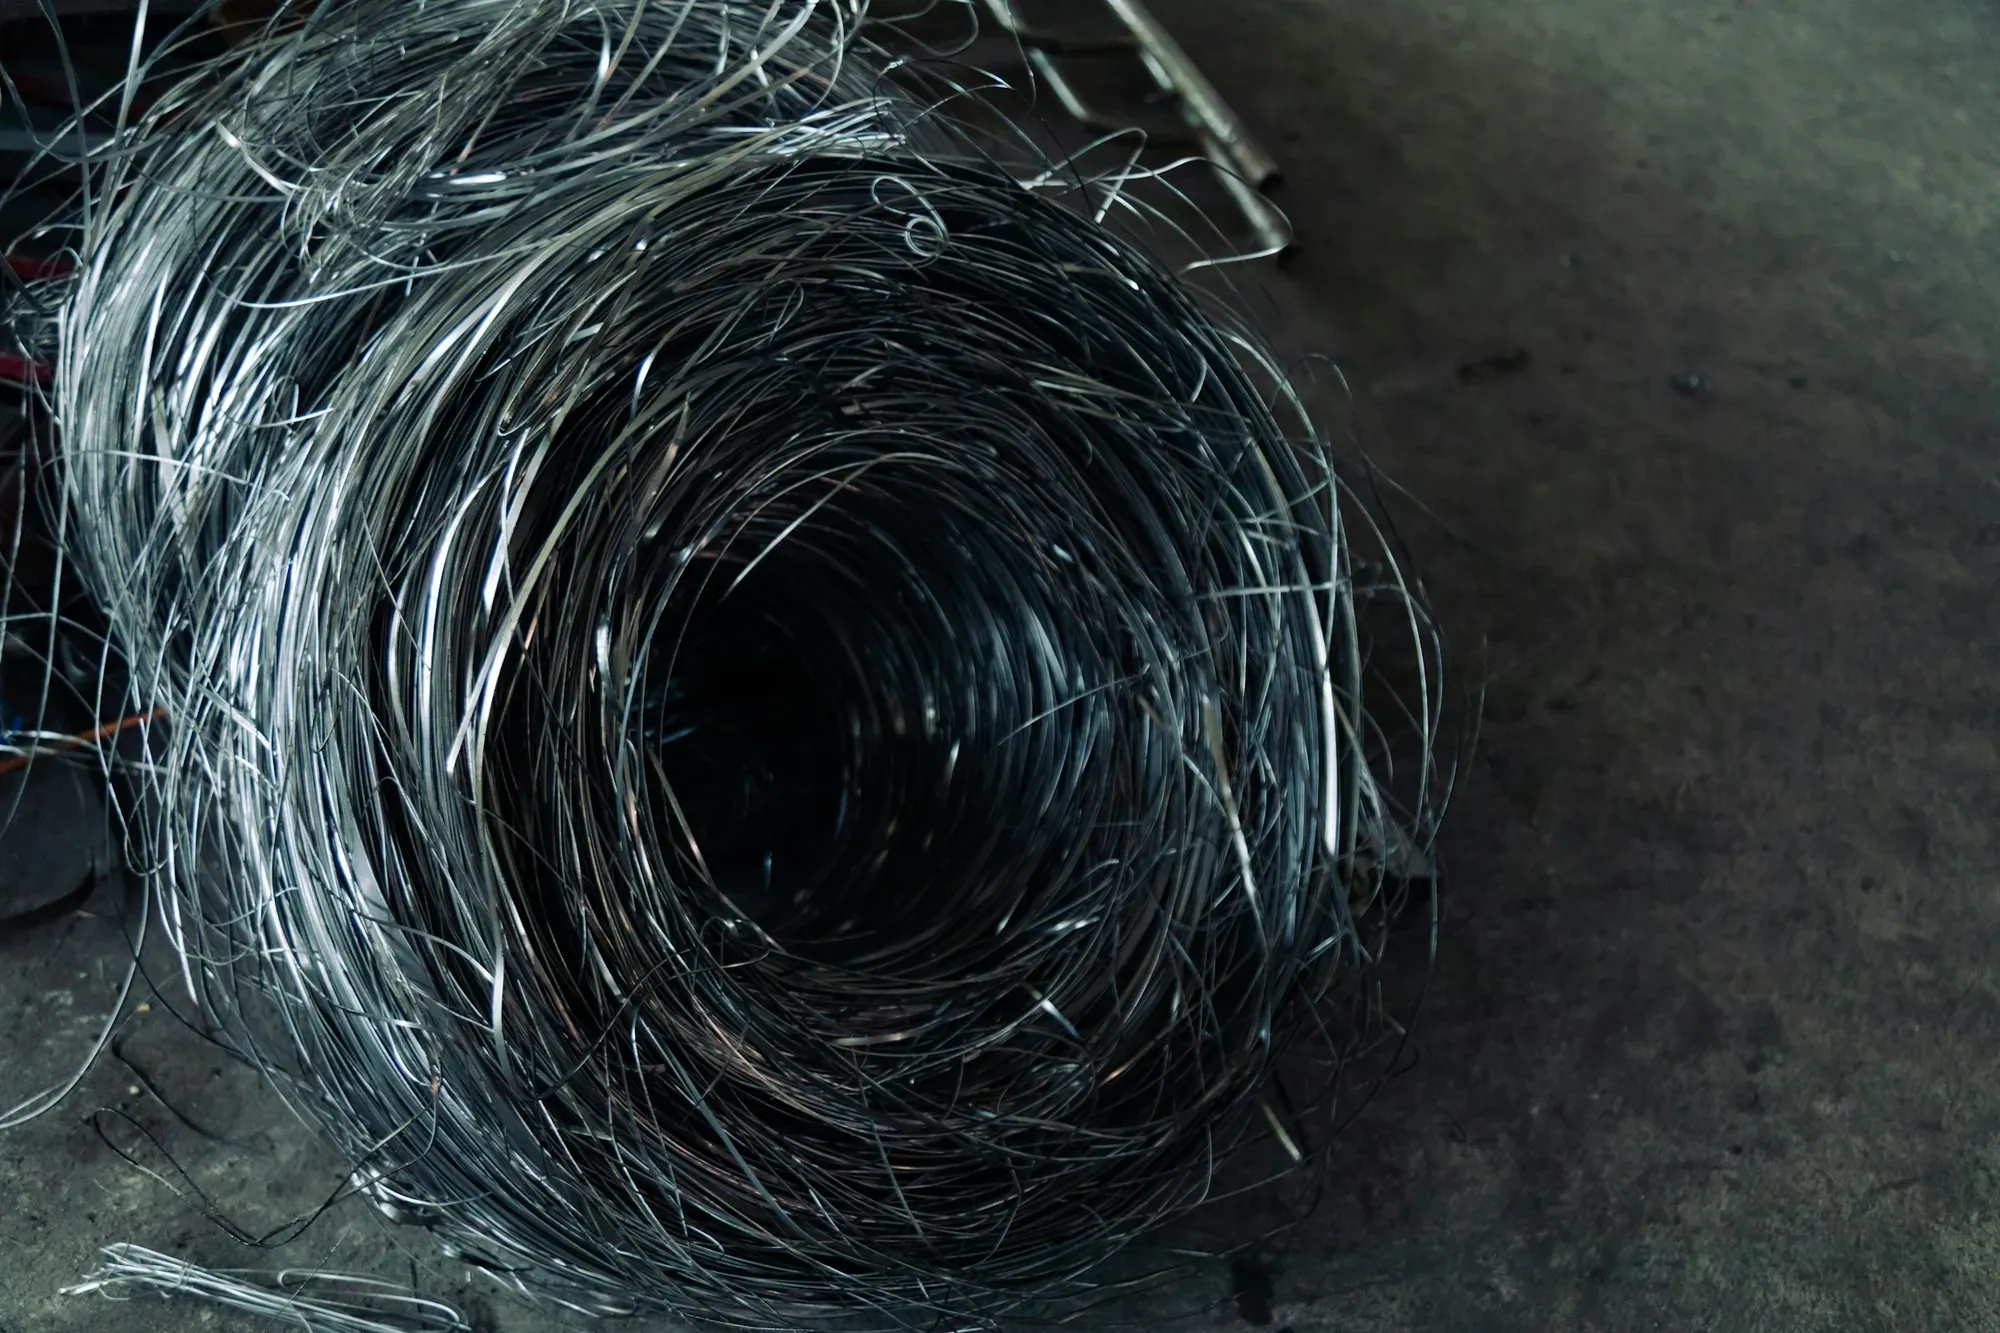
Drawn wire is gauged along the coil and pulled to destruction for tensile and elongation. Gauge is trade shorthand — the millimetre is what is measured, and what the coil is certified to.
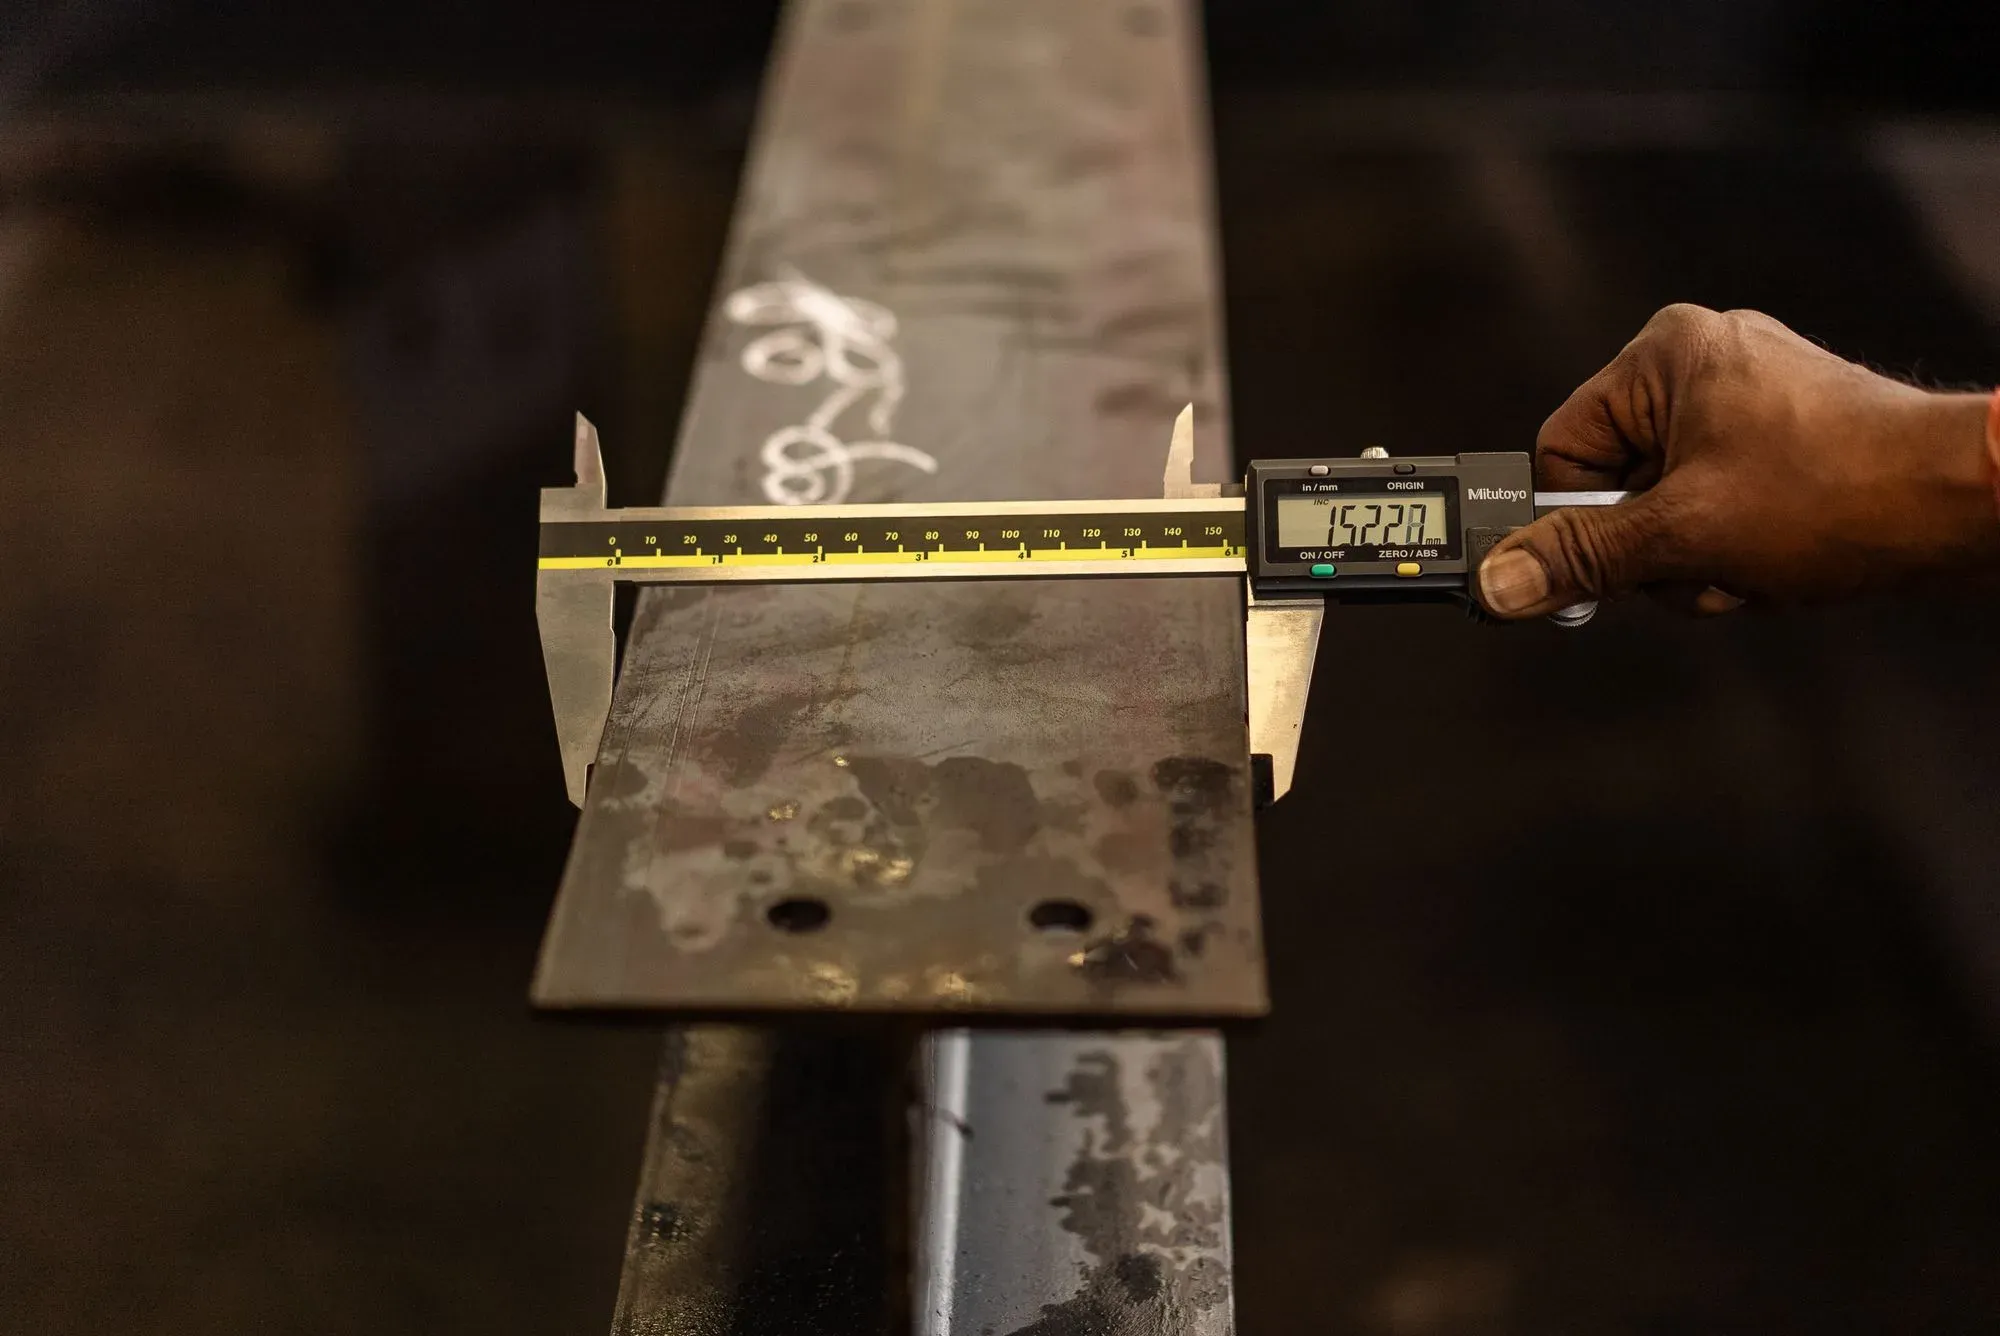
A lux meter checks light levels where dimensional and surface checks are made. A gauge reading and a surface inspection are only as good as the light they are made under, so the light is measured too.
How it is made
Six stages, every one of them inspected. Nothing leaves the mill without a certificate against the standard it was ordered to.
Prime mild steel, galvanized or pre-painted coil is checked for gauge, width and surface before it is accepted onto the floor.
Coil is slit to the strip width the finished profile calls for, so the cover width lands where the drawing says it should.
Strip runs through the forming stands to corrugated, trapezoidal, IBR or tile profile — or through the draw blocks, for wire.
Profiled sheet is cut to the length ordered rather than a standard length, which is what removes end laps from a long run.
Sheet leaves plain, galvanized or colour-coated. Wire is drawn to gauge and then left hard, annealed soft, or zinc coated.
Gauge, coating mass, cover width and tensile checked, and the mill certificate raised against the consignment.
Documentation
Every consignment leaves with a mill test certificate naming the heat, the specification, the dimensional results and the hydro test result. For export orders we add packing lists, certificates of origin and any third-party inspection release the buyer requires.
If your project needs documentation in a particular format — a client's own QA template, an inspection and test plan signed off before production starts — send it through at the enquiry stage rather than at dispatch, and we will build the run around it.
Tell us the specification and the inspection regime at enquiry, and we will confirm in writing what we can certify to before you place the order.
Tell us what you need and it opens in WhatsApp, already addressed. Pick a subject: